Food and Beverage Manufacturer
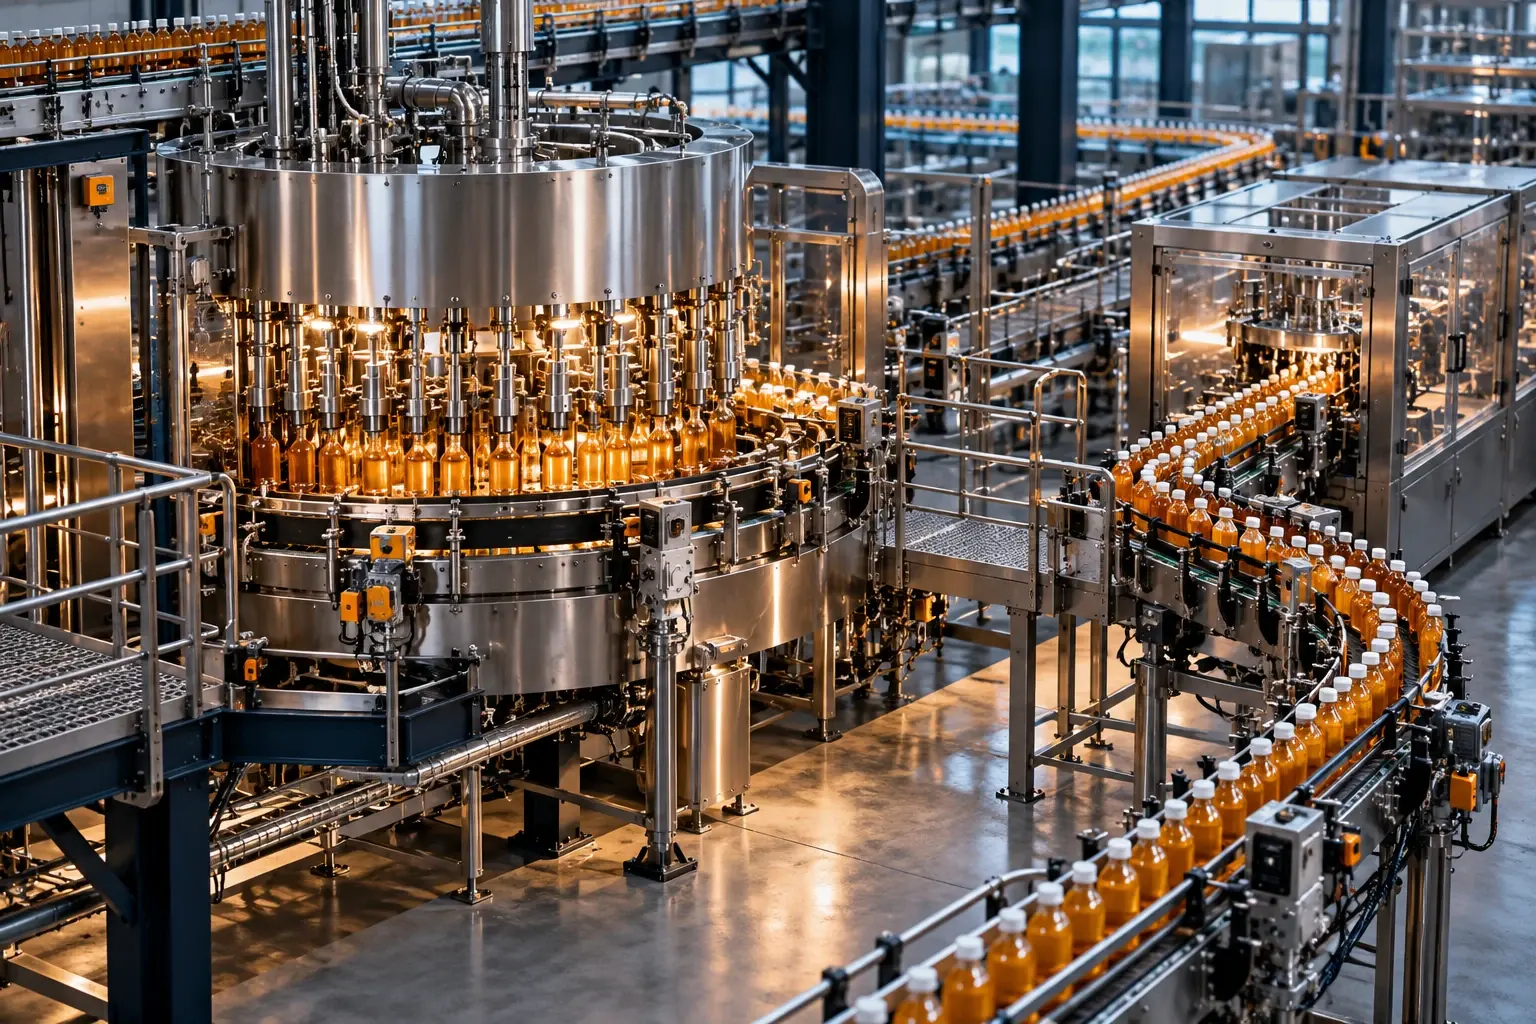
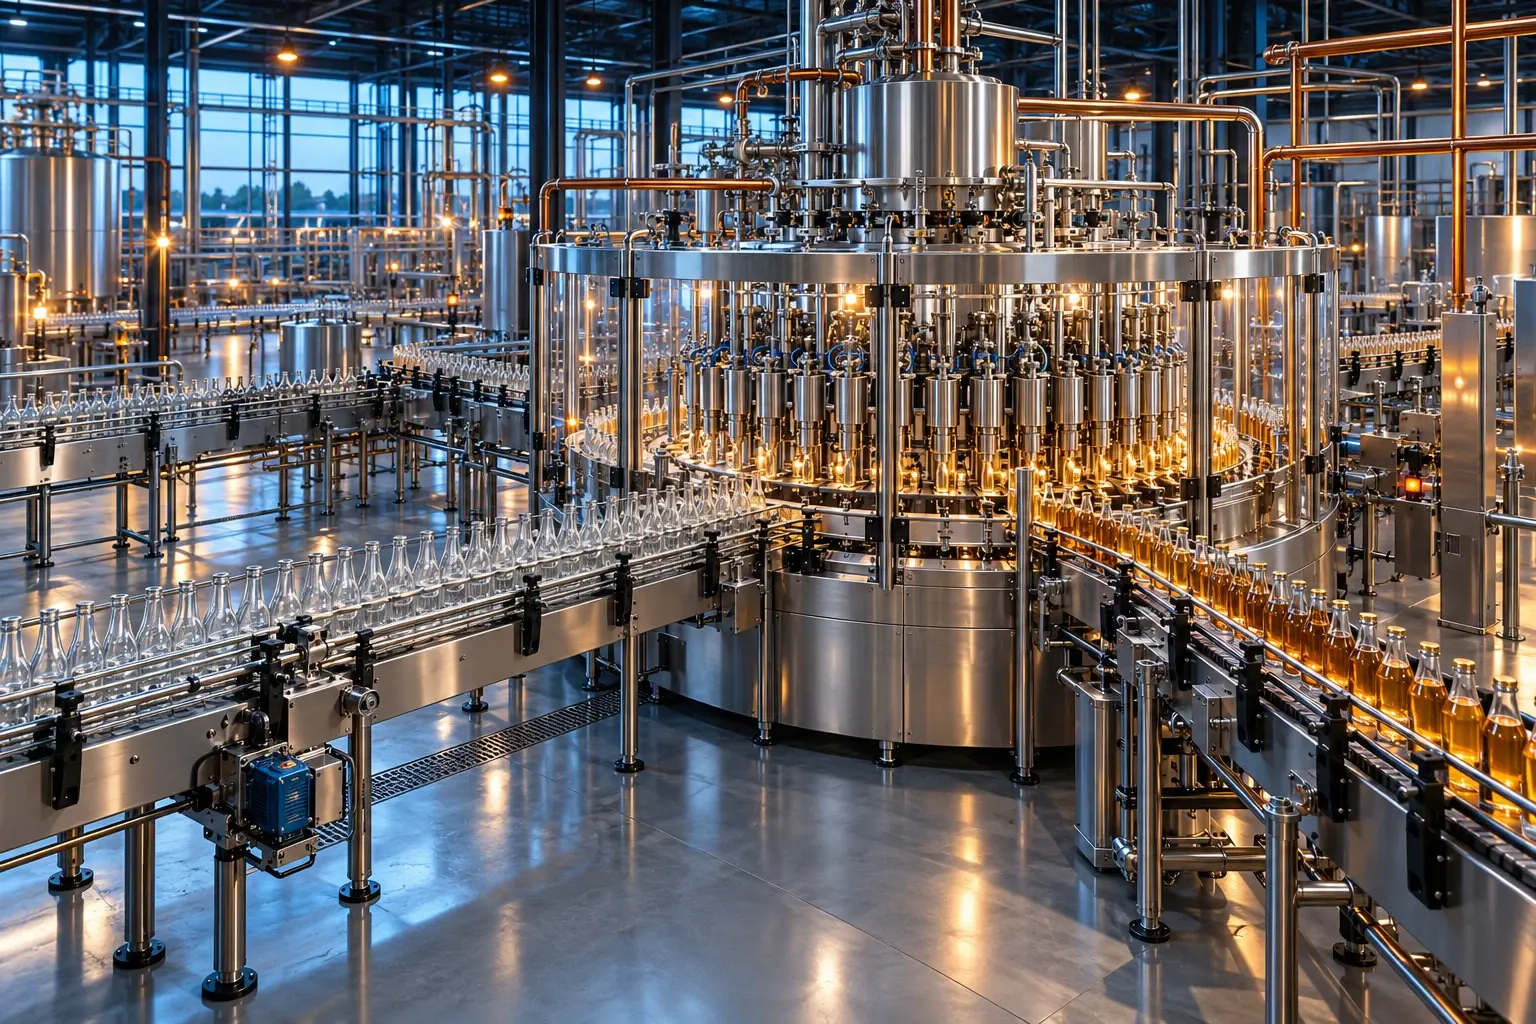
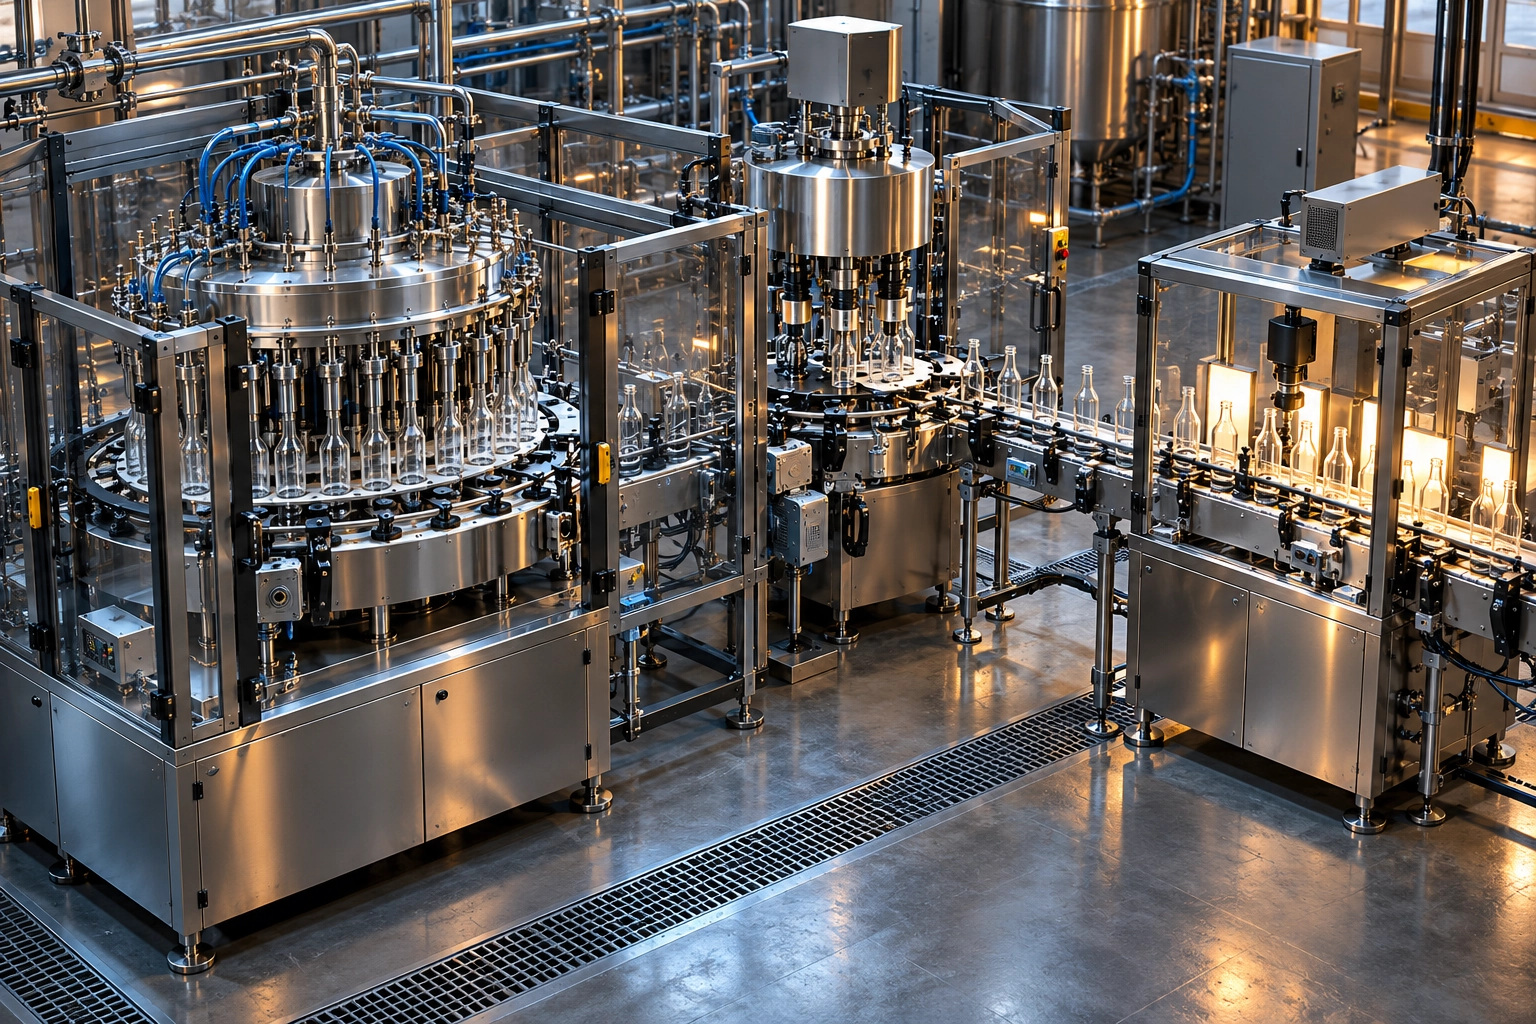
Line 1 Filler and Conveyor Upgrade
Owned the full project lifecycle, from capital planning through commissioning and post-startup support. The filler and conveyor had to operate as one packaging system.
APOLLO AUTOMATIONJAMES WARREN · ENGINEERING & PROJECT LEADERSHIPCASE-064 · Engineering case
A focused hygienic filler retrofit improved throughput while protecting product quality and the operating rhythm of an existing packaging line.

Improve throughput between 35 and 71 percent across SKUs by retrofitting hygienic filler valves and adding return capacity.
Engineering scope: Bottling & Packaging Systems.
Throughput improved by approximately 35–71% across the recorded SKUs. Recorded production examples include 120 BPM for 64 oz, 60 BPM for 128 oz, and 125 BPM for 750 mL.
Workstream Portfolio Rollup
28,095,000 USD
Production and Packaging Modernization
Recorded workstream portfolio reference. This is the workstream-level value and is not a project expenditure or a new total of reassigned projects.
Improved throughput between approximately 35 and 71 percent across SKUs by retrofitting hygienic filler valves and adding return capacity.
Project scope and individual work packages are presented separately; project totals are not additive to their component values.
1 detail rows; 230 K project-family value.
ACTIVITIES IN CONTEXT

TSK-000138 · Technical context
Line 1 Filler and Conveyor Upgrade
Full lifecycle project ownership
Owned the full project lifecycle: capital planning and prioritization, need definition, feasibility and scope development, engineering and AFE justification, procurement and vendor coordination, construction sequencing and field oversight, commissioning, turnover, and post-startup support. Connected operating requirements with technical scope, funding decisions, execution readiness, and the needs of operations and maintenance.
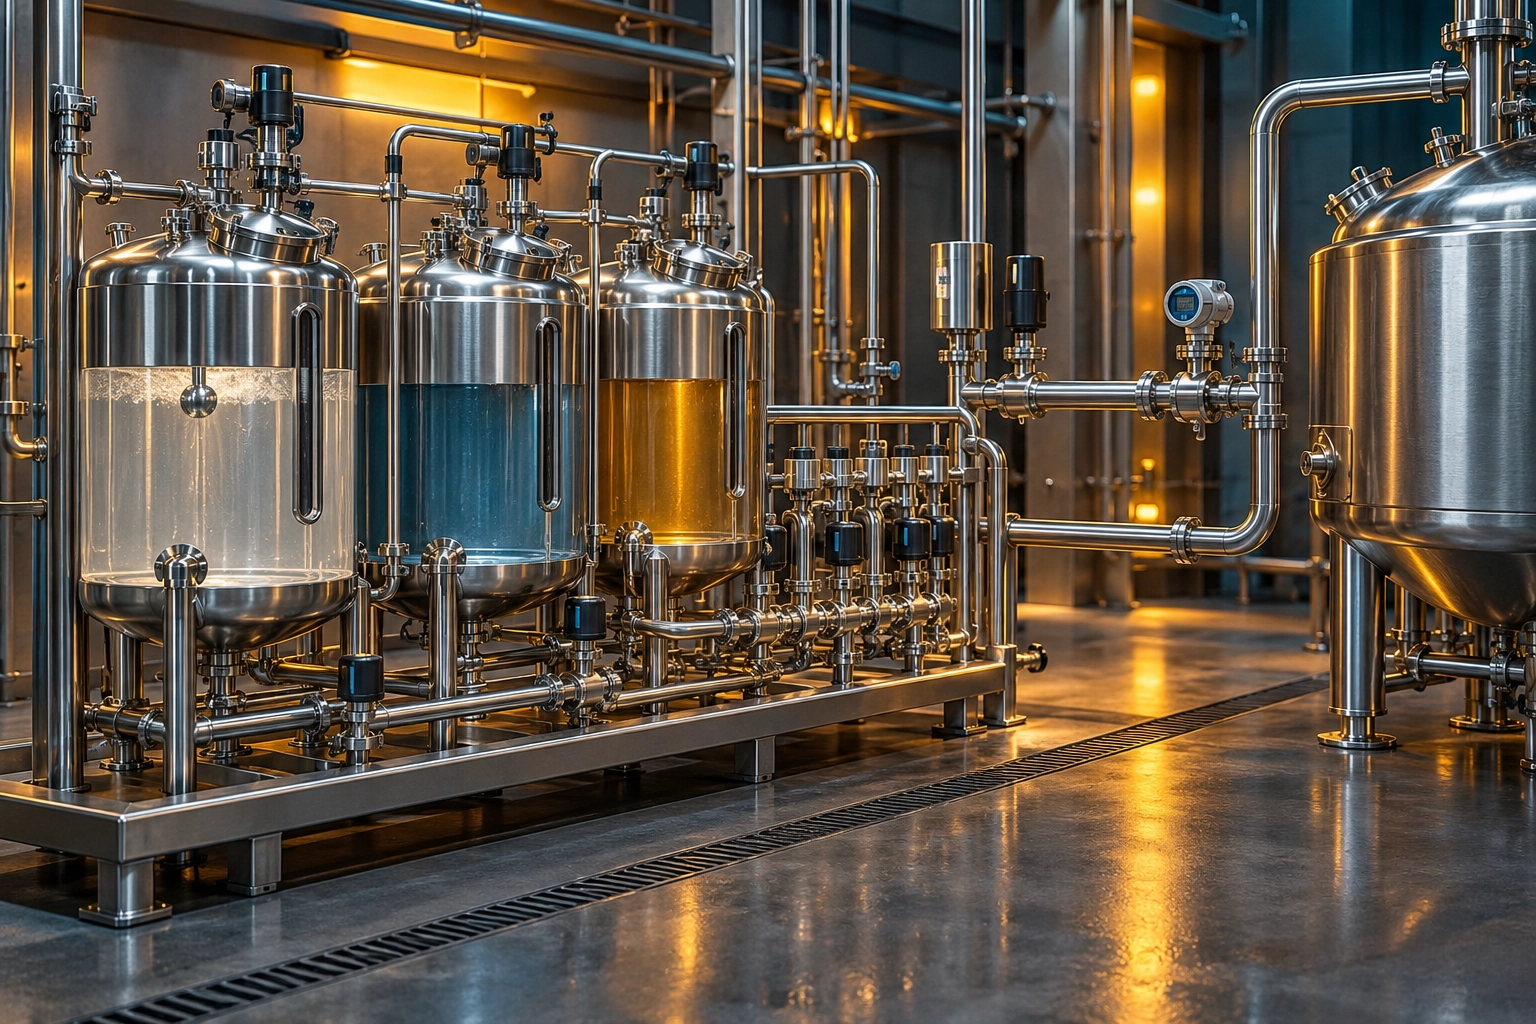
Led the 44-valve hygienic retrofit and coordinated return capacity with conveyor behavior and product supply. Used SKU-level operating evidence to compare performance, keeping the improvement tied to the actual package mix. The engineering connected line capacity with sanitation, maintainability and production continuity.